Introduction to Mold Design for Injection Molding
By Ichiplas Tooling Team · Feb 2024 · Updated Nov 2026 · Reviewed by the Ichiplas engineering team
Mold design is the backbone of efficient and effective plastic injection molding. A well-designed mold ensures high-quality parts, optimizes production efficiency, and minimizes waste. We provide an in-depth look at the fundamentals of mold design, covering mold types, runner systems, gate design, cooling systems, and practical considerations.
Mold Basics
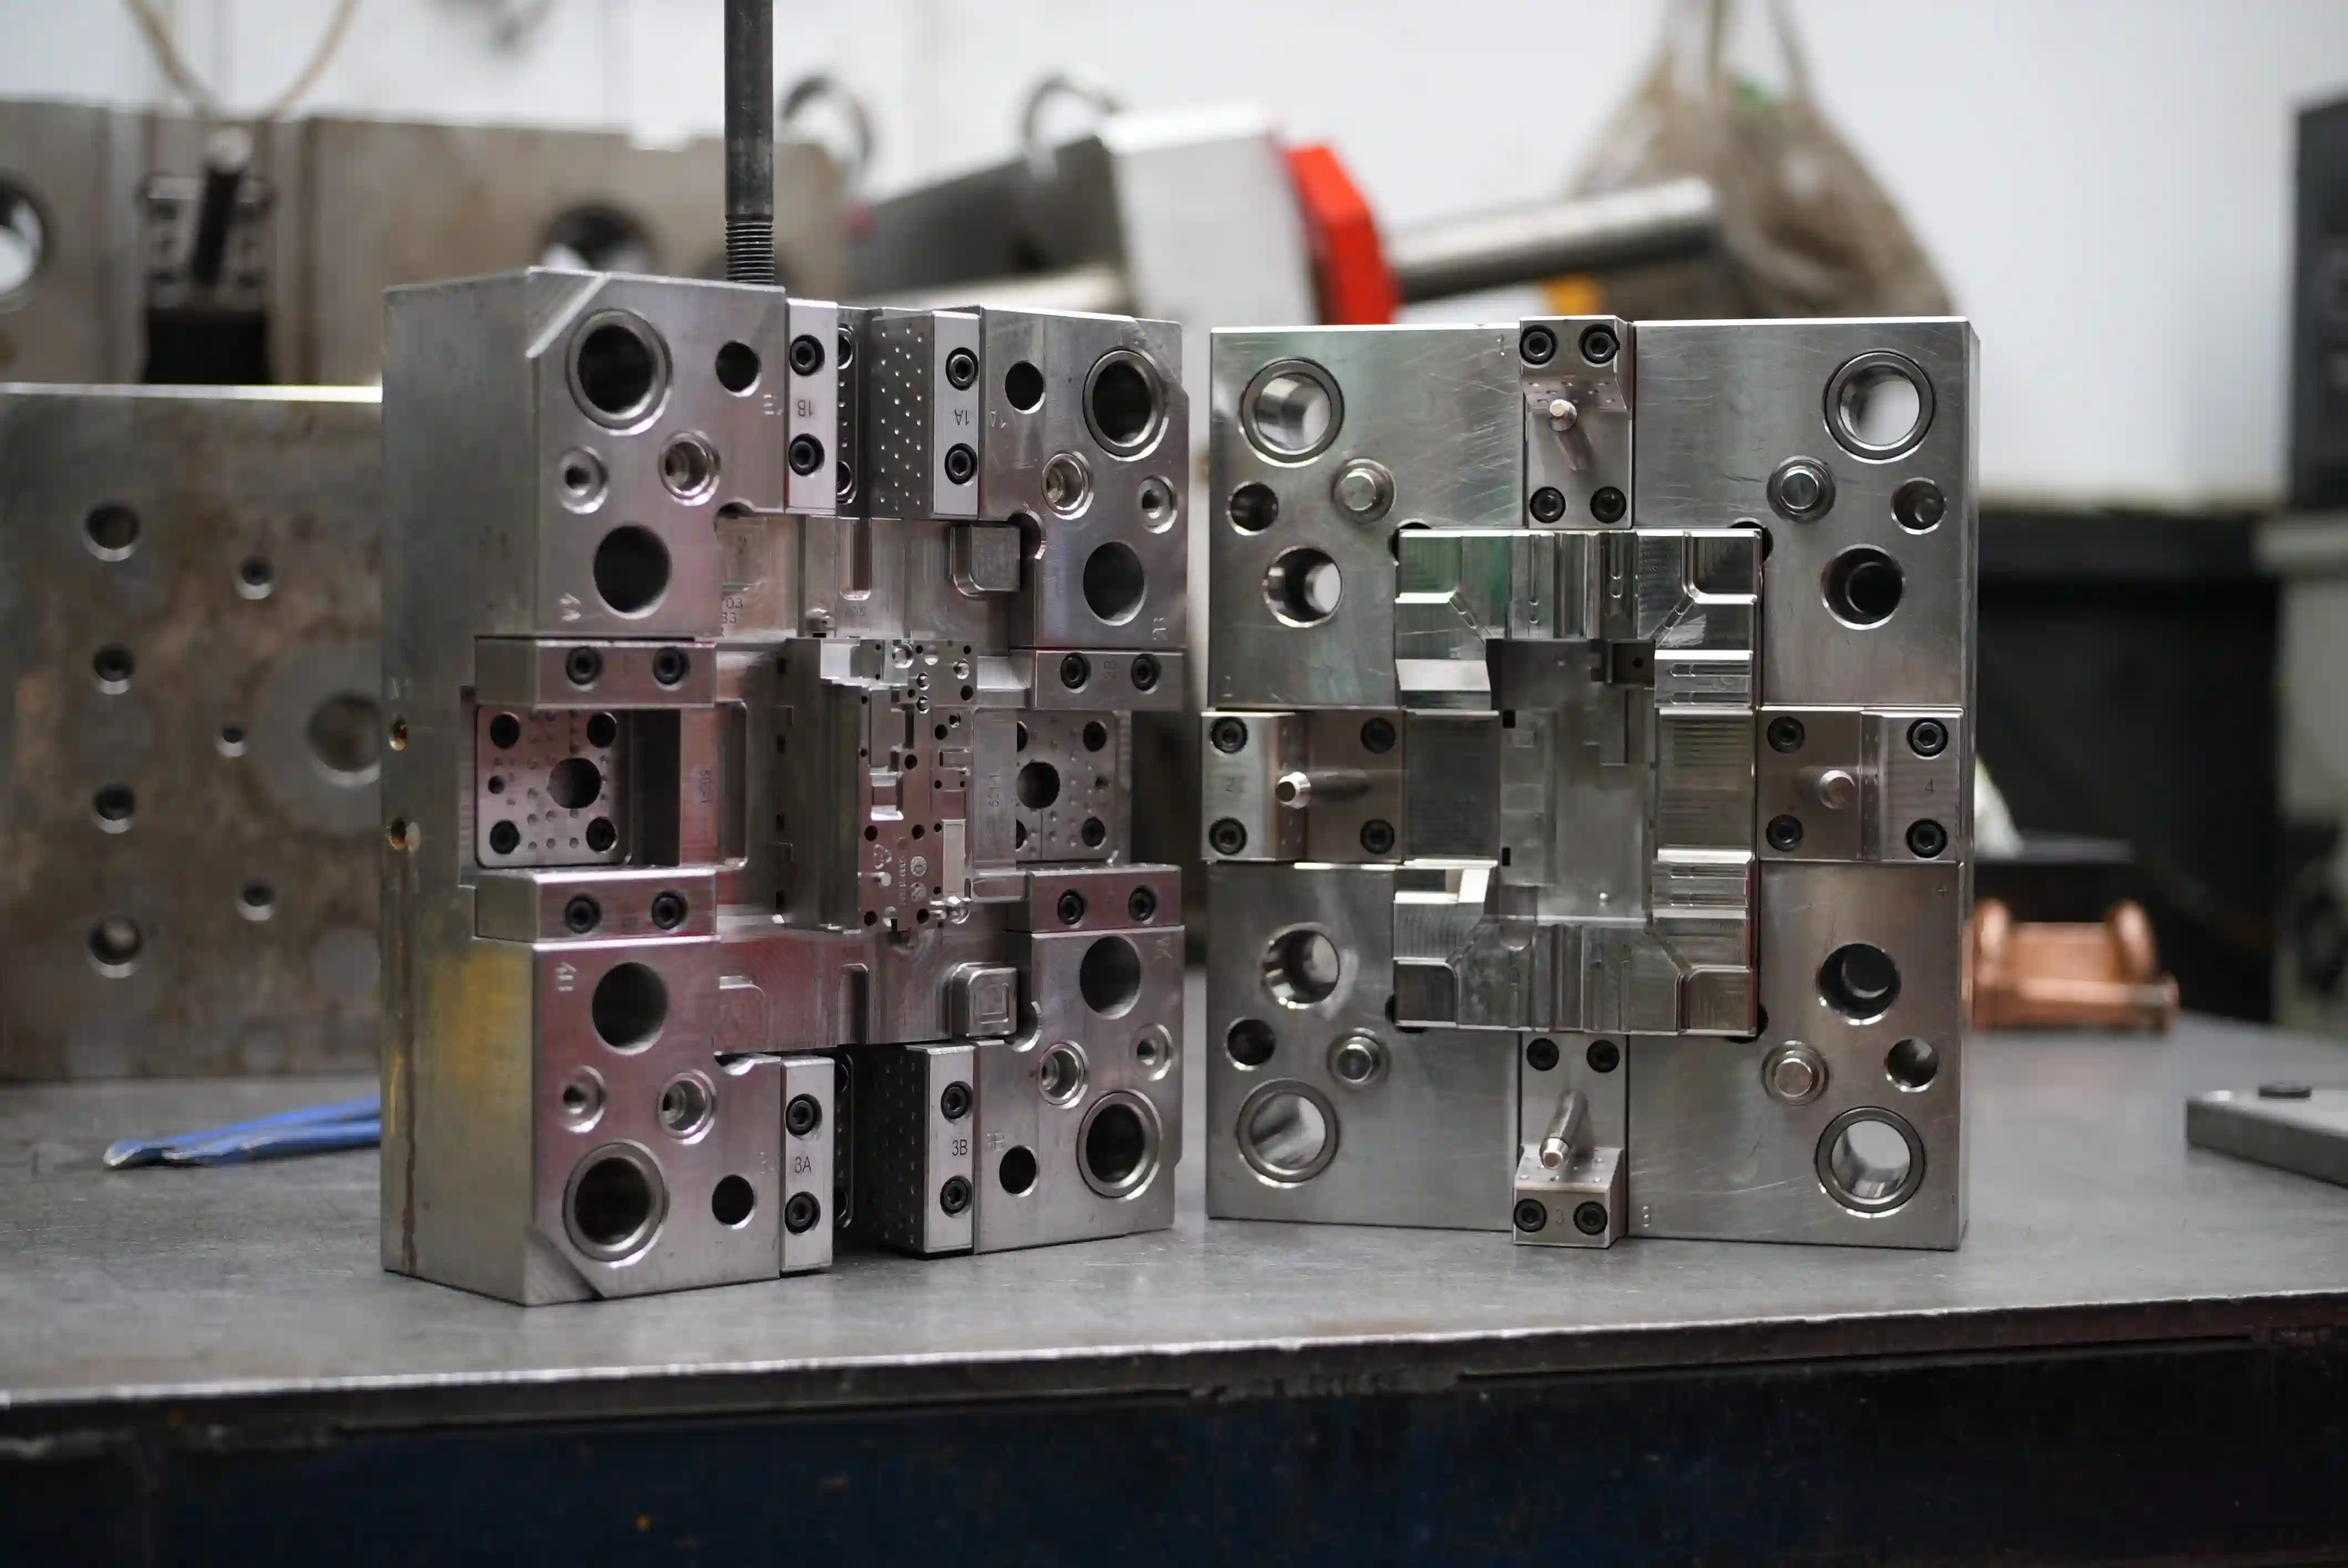
A mold is a precision tool designed to shape molten plastic into desired forms. It consists of two primary sections:
- Fixed Half (Stationary Mold): Houses components such as the sprue bushing and the runner system. This part stays attached to the injection molding machine.
- Moving Half (Dynamic Mold): Includes the cavity plate, core, and ejection mechanism for part removal. It opens and closes during each molding cycle.
Key components of a mold include:
- Injection System: This system guides the molten plastic into the mold cavity through a series of channels:
- Sprue Bushing: The entry point for molten plastic from the machine nozzle.
- Runner System: Distributes plastic evenly to the cavities.
- Gate: Controls the flow of plastic into the mold cavity.
- Cooling System: Regulates the mold’s temperature to solidify the plastic efficiently and uniformly.
- Ejection System: Pushes the cooled, solidified part out of the mold.
For Plastic Injection Manufacturing
Types of Molds
Molds come in various designs, each suited to specific applications. Here are the most commonly used molds:
- 1. Standard Two-Plate Mold
- Introduction:Simplest design with two main sections: the fixed half and the moving half.
- Use Case:Suitable for non-complex parts.
- Example:Simple containers or housings.
- 2. Three-Plate Mold
- Introduction:Includes an additional plate to separate the runner and gate system from the molded part.
- Use Case:Ideal for parts requiring precise gating and minimal visible gate marks.
- Example:Caps, lids, or cosmetic packaging.
- 3. Hot Runner Mold
- Introduction:Utilizes a heated manifold system to keep the plastic molten during injection.
- Use Case:Best for high-volume production and parts with complex gating needs.
- Example:Automotive components or intricate medical devices.
- 4. Family Mold
- Introduction:Designed to produce multiple different parts in a single cycle, using shared runners and gates.
- Use Case:Suitable for sets of related components with similar material requirements.
- Example:Toy parts or multi-component assemblies.
- 5. Insert Mold
- Introduction:Allows for pre-formed inserts, such as metal components, to be placed in the mold before injection.
- Use Case:Ideal for parts requiring additional strength or functional features.
- Example:Threaded inserts or overmolded electrical connectors.
- 6. Stack Mold
- Introduction:Features multiple levels or cavities to double or triple the output per cycle.
- Use Case:Suitable for high-volume production where efficiency is key.
- Example:Packaging items like bottle caps or containers.
- 7. Rotational Mold
- Introduction:Uses a rotating mechanism to facilitate multi-material or multi-color injection.
- Use Case:Best for parts requiring complex designs or color separations.
- Example:Dual-color toothbrush handles or automotive trims.
- 8. Compression Mold
- Introduction:Involves compressing the material in a heated cavity to form the part.
- Use Case:Suitable for thermosetting plastics or rubber components.
- Example:Electrical insulators or automotive gaskets.
Runner System Design
The runner system channels molten plastic to the mold cavities. Its design significantly affects efficiency and part quality.
- Runner Design Considerations: Oversized runners mean easier plastic flow, but more waste material, longer cooling times, and extended cycle times. Undersized runners help save plastic material, but mean higher pressure drops and may lead to inconsistent cavity filling.
- Runner Cross-Sections: Round cross-sections are most efficient, ensuring smooth plastic flow and minimizing freeze-off. Semi-round cross-sections are easier to machine but slightly less efficient. Trapezoidal ones offer a balance between manufacturability and efficiency.
- Efficiency of Runners: Efficiency formula: Efficiency = (Cross-sectional Area) / (Periphery Length). This means round runners provide maximum flow efficiency with minimum cooling issues.
Gate Design
Gates control the flow of molten plastic into the cavity and impact part quality, cycle time, and finishing. Types of Gates include:
- Direct Gates: High flow rates; used for large parts.
- Edge Gates: Ideal for flat parts; leave visible marks on edges.
- Fan Gates: Distribute plastic evenly; great for thin-walled parts.
- Submarine/Tunnel Gates: Trim themselves automatically; ideal for small, complex parts.
Gate sizing also plays a role in the final quality of the parts.
Pressure drops and freezing times must be optimized to prevent short shots (incomplete filling).
Material-specific shear rate limits must also be considered. Shear rate refers to how quickly layers of molten plastic slide over each other as they flow through the gate. Excessive shear can degrade material properties, causing defects like brittleness or discoloration.
Higher shear rate limits indicate a material’s ability to withstand higher flow speeds without breaking down. For example:
- Polypropylene (PP): Handles up to 100,000 shear rate, making it suitable for high-speed molding.
- ABS: Can handle up to 60,000, but beyond this, its properties may degrade.
- Polycarbonate (PC): Has a lower limit of 40,000-50,000 due to its sensitivity to heat.
- PVC: Limited to 15,000 due to its tendency to degrade under heat and shear stress.
Higher isn’t always better. The goal is to match the shear rate to the material’s limits to avoid defects like burn marks or brittleness while maintaining efficient flow.
Cooling System Design
Efficient cooling minimizes cycle time and ensures dimensional accuracy.
- Key Principles: Uniform cooling prevents warping and dimensional inaccuracies. Ideal temperature differentials are 1°C for precision parts and up to 5°C for standard parts.
- Cooling Line Placement: Place channels 2-2.5 times their diameter from the cavity. Use larger cooling channels for thicker parts.
- Advanced Cooling Solutions: Conformal cooling channels adapt to complex part geometries. Common in high-performance molds for electronics and automotive components.
Practical Considerations
Last but not least, other practical considerations include temperature control, air venting, and more.
- Mold Temperature Control: Insulation sheets reduce heat loss. Maintain consistent mold temperature to ensure dimensional stability.
- Air Venting: Proper venting prevents burn marks and air traps. Air vent depth is critical to allow trapped air to escape without plastic leakage. Typical depths vary by material, such as 0.02-0.03mm for PP/Nylon and 0.04-0.06mm for PC. Too shallow and air remains trapped; too deep and plastic flashes through vents.
- Special Notes for Nylon Processing: Ensure proper drying and dehumidification. Moisture in nylon leads to hydrolysis, degrading material strength during molding. And maintain fast injection speeds for consistent fills.
Choosing a Mold Type
Most projects start as a two-plate cold runner mold. The other types solve specific problems — gate location, volume, multiple parts or multiple materials — at extra cost.
| Mold type | Relative tooling cost | Runner waste | Typical annual volume | Choose it when |
|---|---|---|---|---|
| Two-plate (cold runner) | Lowest | Yes | Any | You can gate from the parting line |
| Three-plate | Moderate | Yes | Low – high | You need a center or top gate without a hot runner |
| Hot runner | High | None | Medium – very high | Volume justifies lower waste and faster cycles |
| Family mold | Moderate | Yes | Low – medium | Several parts share one material and color |
| Stack mold | Very high | Low (usually hot runner) | Very high | Flat parts in huge volumes, such as lids |
| Insert mold | Moderate | Yes | Any | Metal inserts must be molded in |
| Two-shot / rotary mold | Very high | Yes | High | Two materials or colors bonded in one cycle |
Compression molding is used for thermosets and rubber rather than thermoplastics, and is not usually an alternative to an injection mold.
Frequently Asked Questions
What is the difference between a two-plate and a three-plate mold?
A two-plate mold opens at a single parting line, and the runner and part are ejected together, so gates are normally on the part's edge. A three-plate mold adds a runner plate that opens separately, which lets the runner reach pin-point gates anywhere on the part and separates the runner from the parts automatically.
When is a hot runner mold worth the extra cost?
A hot runner usually pays back at higher annual volumes, with expensive resins where runner scrap is costly, with multi-cavity molds where a cold runner would be large, or where gate cosmetics demand a valve gate. For low volumes and simple parts, a cold runner is usually the more economical choice.
What is mold flow analysis and do I need it?
Mold flow analysis is simulation software that predicts how plastic will fill, pack and cool in the mold, showing likely weld lines, air traps, sink and warpage before steel is cut. It is strongly recommended for large, thin-walled, cosmetic or tight-tolerance parts and for choosing gate locations on new designs.
Which steel should my mold be made from?
It depends on volume, resin and finish. Pre-hardened steels such as S50C or P20 suit lower volumes and are quicker to machine; NAK80 gives a good polish for mid-volume cosmetic parts; hardened H13-type steels such as 8407 suit high volumes and abrasive glass-filled resins; and stainless grades such as S136 or Stavax suit optical parts and corrosive resins.
How long does it take to design and build an injection mold?
For a moderately complex single-cavity mold, design and fabrication to first samples (T1) commonly takes about four to eight weeks. Simple molds can be faster, while large, multi-cavity, hot runner or multi-action molds take longer. Your tooling quotation should state a lead time to T1.
Why Choose a Johor Bahru-Based Manufacturer?
Johor Bahru is a hub for high-quality and cost-effective plastic injection molding services. Local manufacturers leverage advanced technologies and proximity to key markets, ensuring timely delivery and competitive pricing. With expertise in handling diverse materials, manufacturers in Johor Bahru are equipped to meet both small and large-scale production needs.
Mold design is a cornerstone of successful plastic injection molding. By understanding basic principles, optimizing mold features, and aligning design choices with part requirements, manufacturers can achieve consistent, high-quality results. By mastering concepts such as shear rates, venting, and cooling, manufacturers ensure every cycle produces reliable parts without defects. Whether you're a beginner or an expert, adhering to these practices elevates your injection molding capabilities. Explore our mold design and fabrication services to see how we put these principles into practice.
Contact us today to discuss your plastic injection molding needs, or if you are thinking of moving your manufacturing base to Malaysia!
Get Free Quote
Contact us today to learn more about our services and how we can help you with your next project.